
Inside Our 13,000 m2 Shot Blasting Machine Factory
Every shot blasting machine we ship is built in our own 13,000 square meter factory in Dafeng, Yancheng, Jiangsu, China. Fabrication, machining, casting, heat treatment, balancing, assembly and testing all run on site, under one quality system and one management team.
That matters when you are buying a machine expected to run for twenty years. When the blast wheel, the blast chamber and the wear parts are made by the same people who build the machine, tolerances line up, replacement parts fit, and one party is accountable for the result.
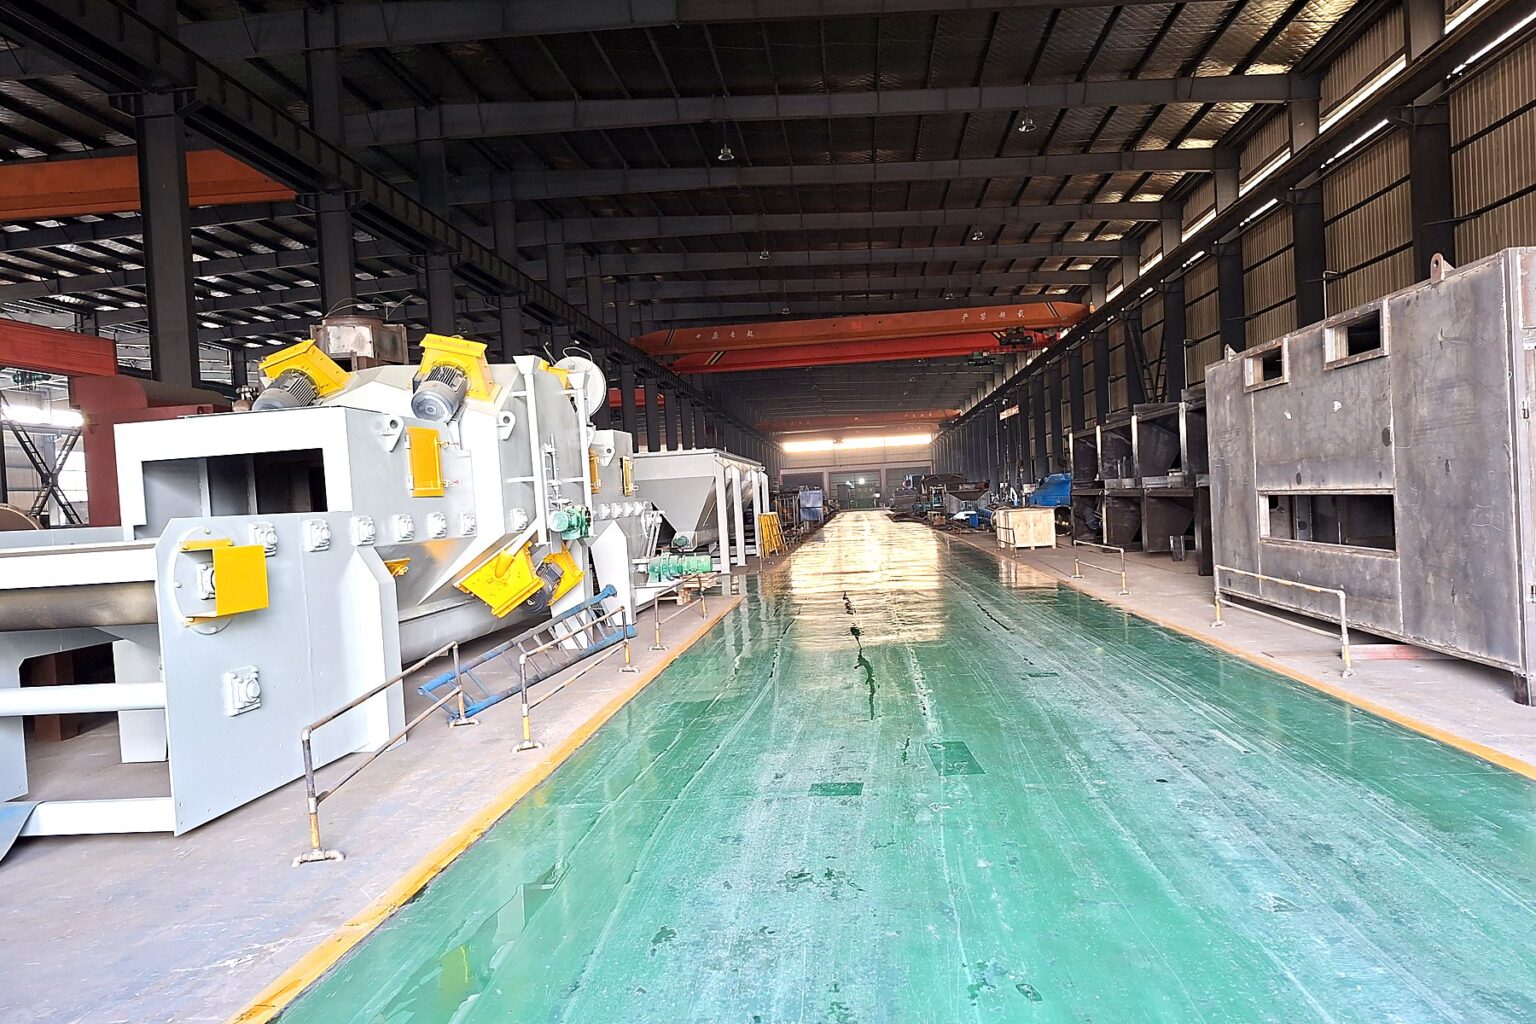
In-House Processes
Most suppliers assemble. We machine, cast, heat treat and balance.
Seven operations that decide how long a shot blasting machine lasts, all running inside one plant.
01 · Laser Cutting
Laser Cutting and Sheet Metal Forming
Steel plate up to 50 mm thick, cut to drawing without thermal distortion. Two high-power laser cutting machines handle the chamber walls and structural plates. Press brakes and shearing machines complete the forming work for housings, hoppers and guards.

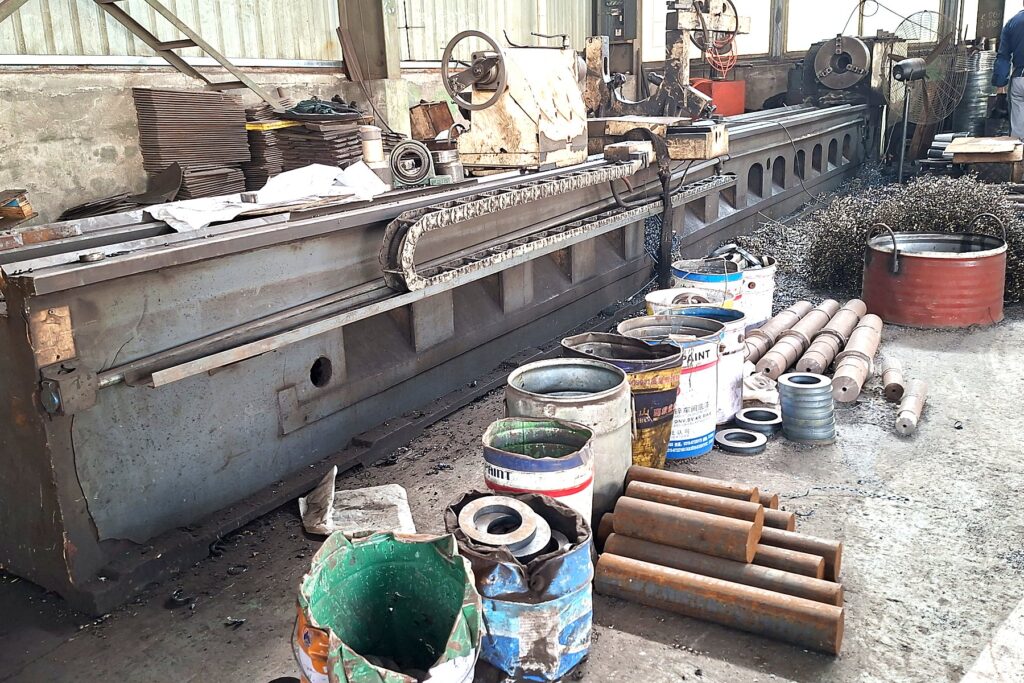
02 · Heavy Machining
Heavy Machining
A heavy lathe that machines workpieces up to 8 meters long. CNC machine tools and machining centers cover the precise work: bearing seats, shaft journals, flange faces and bolt patterns. Separator shafts, conveyor shafts and large diameter rings are turned in a single setup.
04 · In-House Casting
In-House Casting for Wear Parts
We monitor melt chemistry and casting dimensions throughout production. Wear components are selected and processed to suit each machine’s abrasion and impact conditions. We verify material properties, hardness and fit against project requirements to support dependable service life.


05 · Heat Treatment
Heat Treatment
Hardness and toughness set by a recorded cycle. An on-site heat treatment center runs the hardening and tempering processes for cast wear parts. Every batch follows the same recorded curve, so hardness is repeatable from one order to the next.
06 · Dynamic Balancing
Dynamic Balancing
Every blast wheel is balanced before it is fitted. An unbalanced wheel vibrates, wears bearings early and shortens blade life. A dedicated balancing laboratory makes this a standard production step rather than an optional extra.


07 · Laboratory
Physical and Chemical Laboratory
Alloy grade and hardness confirmed by test, not by supplier declaration. Our laboratory verifies material composition and mechanical properties, so the material you receive matches the material specified on the drawing.
07 · Fabrication & Welding
Fabrication and Welding
Chambers, hoppers and frames welded in-house. Structural fabrication runs on site, and critical welds are inspected before the chamber goes for machining. Every machine is assembled and test run before it is dismantled for shipment.

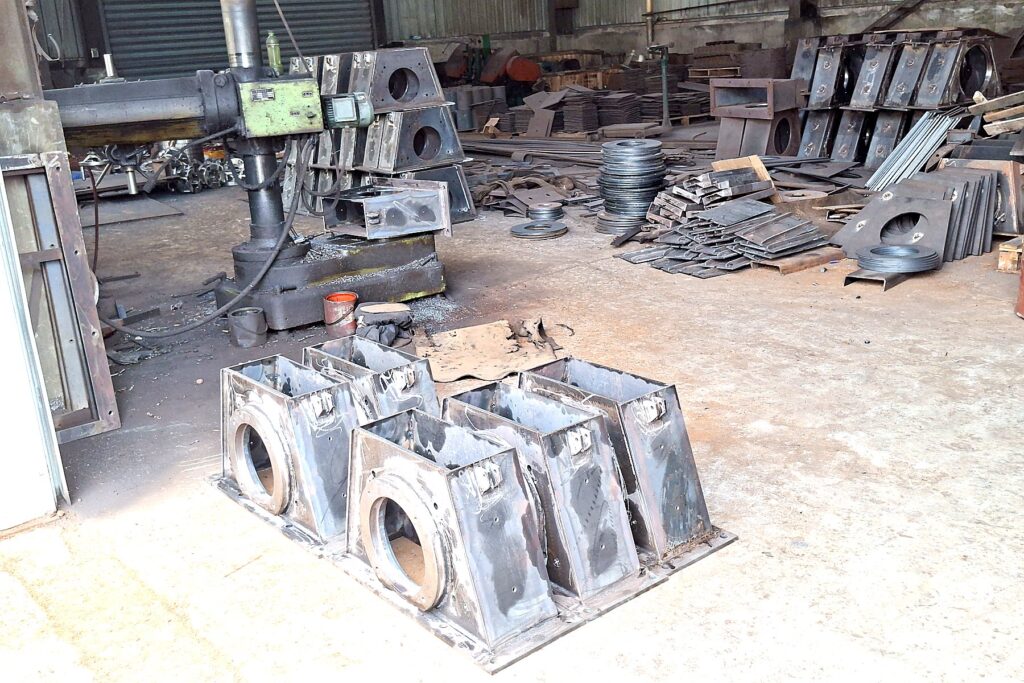
08 · CNC Machining
CNC Machining Center
Bearing seats, flange faces and bolt patterns cut on CNC equipment. Machining centers hold the tolerances that decide whether a blast wheel runs true and whether a replacement part drops straight into place.
09 · Electrical Control
Electrical Control Panels
Control panels wired and tested in our own workshop. Blast wheel drives, abrasive circulation, dust extraction and safety interlocks are assembled and checked in-house, so the machine arrives as one working system rather than a set of parts.

Production Flow
From steel plate to commissioned machine
Six stages, one factory, one quality record per machine.
01
Cutting and Forming
Laser cutting, shearing and press braking produce chamber panels, frames and housings.
02
Welding and Fabrication
Chambers, hoppers and structural frames are welded in-house. Critical welds are inspected.
03
Casting and Heat Treatment
Wear plates, blades, control cages and impellers are cast, heat treated and machined.
04
Machining
Precision parts are turned, milled and drilled on CNC equipment, and on the 8 meter lathe where size requires it.
05
Balancing and Sub-Assembly
Blast wheel assemblies are dynamically balanced, then abrasive circulation systems are assembled and aligned.
06
Assembly, Testing and Painting
The complete machine is assembled, electrically wired, test run, inspected and painted before shipment.
Engineering
Engineering and custom manufacturing
Built to Your Workpiece, Not to a Catalogue
Machine size, chamber opening, conveyor type, blast wheel count and layout are set by your workpiece dimensions, throughput and surface standard. Because fabrication and machining are in-house, custom chamber sizes and conveyor configurations are routine work rather than special projects.
OEM and ODM Manufacturing
We manufacture shot blasting and sandblasting equipment for OEM and ODM programmes, including private label supply for overseas partners. Drawing-based production, agreed inspection points and shipping documentation are handled as part of the standard process.
Turnkey Delivery
Supply covers foundation drawings, machine manufacture, shipment, on-site installation and commissioning, operator training and spare parts supply. Abrasive media, dust collection and coating lines can be included so the surface preparation process is complete at handover.
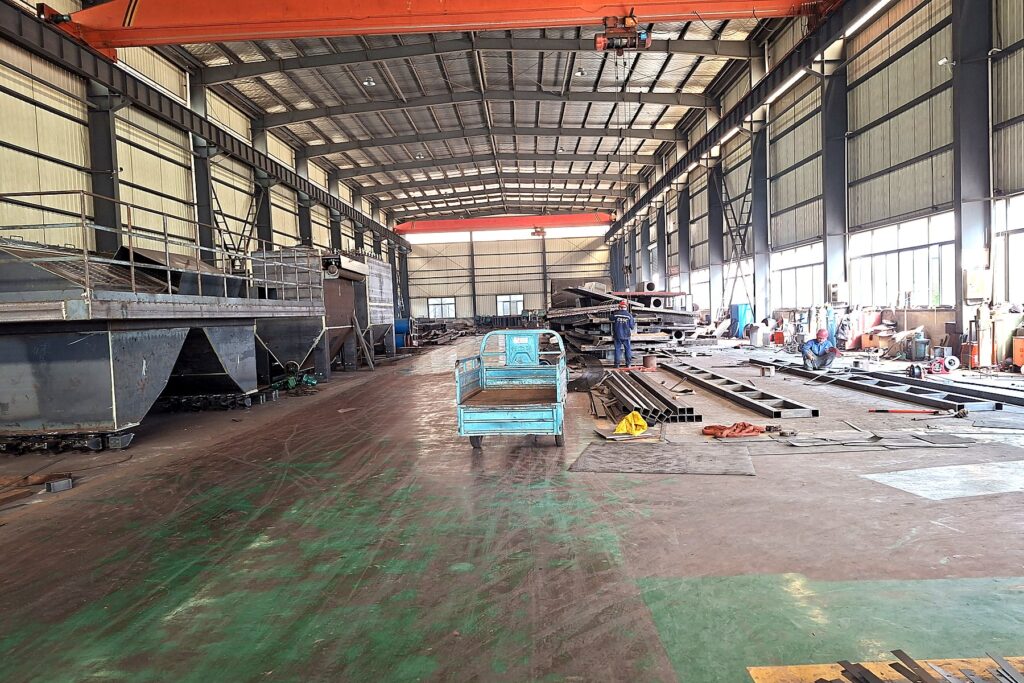
On the Assembly Floor
Tested before it is packed
Blast wheel speed, abrasive circulation, separator performance, dust extraction airflow and safety interlocks are verified on every machine, and the results are documented for the customer file.
Quality
Quality control and inspection
Incoming Material Verification
Steel plate, castings and bought-in components are checked against specification on receipt, including composition and hardness testing in our laboratory.
In-Process Inspection
Critical processes are inspected as they happen, not only at the end. Weld quality, machined dimensions, casting integrity and balancing results are recorded per unit.
Final Test Run Before Shipment
Every machine is assembled and run before it is packed. Wheel speed, abrasive circulation, separator performance, dust extraction airflow and safety interlocks are verified, and the results are documented for the customer file.
Certifications
Certifications and standards
Marine and industrial projects are delivered against the standards our customers specify at tender stage.
- National High-Tech Enterprise
- Customs registered exporter
- ISO 9001
- ISO 8501-1
- ISO 8503
- SSPC-SP10
- CCS (China)
- RINA (Italy)
- Lloyd’s Register (UK)
- IACS member rules
Why Factory-Direct
Why buyers choose a factory-direct manufacturer
One Party Owns the Quality
The alloy in the wear plate, the hardness after heat treatment, the balance of the blast wheel and the finish of the blast chamber are all decided inside one plant. When a part fails early, there is no supplier chain to negotiate with. We test the material, we know the process, and we correct it.
Custom Work Without a Middle Layer
A customized chamber opening, a different conveyor pitch or an unusual blast wheel layout is a drawing change for us, not a negotiation between three companies. That shortens the path from your workpiece dimensions to a machine that fits them.
Factory-Direct Pricing and Faster Spare Parts
There is no trading margin between the workshop and your purchase order, and replacement parts are cast and machined from the same patterns used for the original machine. Shot blasting machine wear parts are consumables, so the cost of the second and third order matters as much as the price of the machine.
Common Questions
Can you manufacture a shot blasting machine to my workpiece dimensions?
Yes. Machine size, chamber opening, conveyor type, blast wheel count and layout are set by your workpiece dimensions, throughput and surface standard.
Send the workpiece drawings, the maximum and minimum dimensions, the required surface cleanliness grade and your target output per shift. Our engineering team prepares a process proposal, and the machine is built to that specification rather than adapted from a standard catalogue model.
What should I check when auditing a shot blasting machine factory?
Check four things: whether the wear parts are cast in-house, whether blast wheels are dynamically balanced, whether there is a heat treatment step with recorded cycles, and whether there is a laboratory that tests material.
Assemblers can buy steel and bolt machines together. Casting, heat treatment, balancing and material testing require plant and people, and they are the operations that determine how long a machine lasts.
How do you control the quality of blast wheel and wear parts?
By controlling the melt and the heat treatment, then measuring the result.
Alloy composition is confirmed in our laboratory before casting. Hardness is checked after heat treatment. Every blast wheel assembly is dynamically balanced before it is fitted, and the balancing result is recorded. Wear parts are gauged against the original mounting dimensions so they install without modification.
Do you supply spare parts after the warranty period?
Yes. We manufacture compatible wear parts and spare parts for our own machines and for Wheelabrator, Pangborn and Sintokogio (Sinto) equipment, so a machine bought today can still be maintained a decade from now.
Blades, control cages, impellers, blast chamber wear liners, feed pipes, sealing curtains and dust collector filter cartridges are all produced from our own patterns.
Which industries do your shot blasting machines serve?
Structural steel fabrication, shipbuilding and marine construction, wind turbine tower manufacturing, foundries, forging, steel pipe and OCTG production, automotive and brake component manufacturing, and stone surface texturing.
Each industry sets different requirements for chamber size, conveyor type and blast pattern, which is why machines are configured per project rather than sold from stock.
How do I get a quotation, and how long does delivery take?
Send your workpiece details, the required surface standard and your target output, and our engineering team prepares a process proposal and quotation, normally within 24 hours.
Standard machines are typically delivered in 30 to 60 days depending on configuration and quantity. Custom chambers and lines take longer, and the schedule is confirmed in the order.
Visit
Visit our factory
Buying a shot blasting machine is a long-term decision, and it is reasonable to want to see where it is made. We welcome factory visits, and for overseas customers we can arrange a live video walk through the workshop covering the machining area, casting and heat treatment, the balancing laboratory and the assembly bay.
Send us your workpiece details and we will prepare a process proposal and a quotation. Our engineering team normally responds within 24 hours.
Email: dtcx@dt-shotblasting.com
WhatsApp / WeChat: +86 15895165618
Website: https://dt-shotblasting.com/
More About Our Machines and Wear Parts
• shot blasting machine wear parts for all major brands
• Wheelabrator compatible spare parts