This guide is written for process engineers, equipment managers, and procurement teams in foundries, heat treatment plants, automotive and specialty vehicle frame manufacturing, coal mine hydraulic support production, steel structure fabrication, and powder coating (painting) line operations. It covers the full lifecycle of the monorail continuous pass-through shot blasting machine (continuous overhead monorail shot blasting machine) — from selection and installation to daily maintenance and troubleshooting.
Monorail continuous pass-through shot blasting machine in operation at a customer site
Data Note: Values marked “industry reference” are ranges from public sources and engineering experience, intended for preliminary evaluation. For formal procurement and process acceptance, the manufacturer’s technical documentation, mutually confirmed process test results, and current valid standards shall prevail.
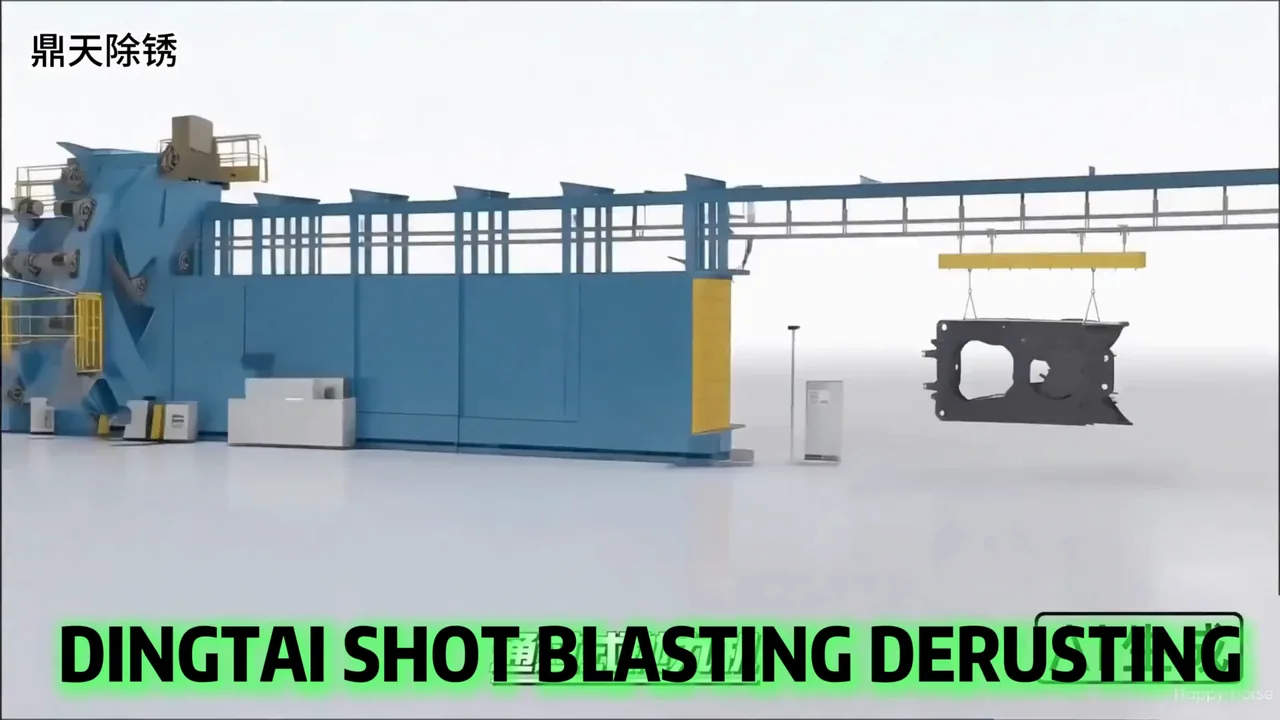
Workpieces are hung on fixtures suspended from an overhead monorail chain. The chain carries them continuously or intermittently through a shot blasting chamber, where multiple high-speed rotating blast wheels project abrasive media onto the workpiece surface from different spatial angles — completing sand removal, rust removal, descaling, and surface texturing in a single pass.
Continuous High-Volume Processing: Workpieces circulate on the chain; loading/unloading and blasting can be independently partitioned. Stable cycle times make it ideal for large-scale production.
Omnidirectional Coverage: Workpieces rotate or oscillate while suspended; combined with multi-angle blast wheel arrangement, this handles bottom surfaces, internal cavities, and complex contours that roller conveyor machines cannot reach.
Direct Line Integration: The overhead conveying system is naturally suited for sharing the same suspension chain with powder coating and painting lines, achieving integrated “shot blasting → blow-off → spraying → curing” flow.
1.2 Differences from Adjacent Models (Clarify Before Selection)
Domestic monorail cleaning equipment is typically divided into three categories by conveyor chain operation mode (model prefixes vary by manufacturer; procurement should be based on operation mode rather than model number). All three are variants of the monorail conveyor shot blasting machine:
Push chain and load-bearing chain separated; fixtures can accumulate and stop at designated zones
Buffering between processes, decoupling from coating line cycle times
Selection Tip: If the shot blasting process shares a monorail with a downstream coating line and the two processes have different cycle times, the indexing monorail shot blasting machine is almost mandatory — it allows workpieces to accumulate at the blasting chamber exit and wait, preventing the entire line from being dragged to a stop.
For most buyers, however, the decisive factor is not brand prestige but total cost of ownership at equal cleaning performance. On comparable specifications — similar blast wheel power, similar hanger load, similar achievable cleanliness grade (Sa2.5) — a Chinese monorail shot blasting machine is typically available at roughly one-third of the price of equipment from German Wheelabrator, US Pangborn, or Japanese Sintokogio (New East), while delivering equivalent cleaning quality on the same workpiece types.
Note on equivalence: “Equivalent quality” here refers to the achievable surface cleanliness grade, roughness range, and cleaning coverage on the same workpiece under the same abrasive and speed conditions. Buyers should always confirm equivalence through actual workpiece process validation (see Section 5), not through brochure claims alone — regardless of whether the machine carries the German Wheelabrator name, the US Pangborn name, the Japanese Sintokogio (New East) name, or any other brand.
Understanding the structure is the prerequisite for good selection and maintenance. A complete monorail conveyor shot blasting machine typically consists of six subsystems.
Drive unit: Variable-frequency speed control for stepless adjustment of conveying speed.
Tensioning device: Counterweight or spring tensioning to absorb chain thermal elongation and wear elongation.
Fixtures and rotation mechanism: Hooks, hanging beams; some models feature planetary rotation (rotation + revolution simultaneously) to ensure uniform abrasive coverage on all surfaces, avoiding “shadow” effects.
Turning and climbing sections: Determine factory layout and chain length.
2.2 Blasting Chamber & Blast Wheels
Chamber: Steel plate welded structure with high-chromium wear-resistant liners (or Mn13 liners) on inner walls; liners are replaceable sacrificial components.
Blast wheels: Cantilever centrifugal blast wheels are mainstream, consisting of motor, impeller, abrasive distributor, directional sleeve, blades, and liners. The number, power, installation angle, and spatial position of blast wheels determine cleaning coverage; reputable manufacturers determine arrangement through 3D dynamic projection simulation.
Sealing devices: Multi-layer rubber curtains or labyrinth seals at inlet/outlet to prevent abrasive escape.
2.3 Supplementary Blasting Chamber (Key Design for Extra-Large Workpieces)
For workpieces such as truck chassis frames and coal mine hydraulic supports with large dimensions, complex structures, internal cavities, and dead zones, fixed projection angles from the main blasting chamber alone cannot achieve full coverage. Therefore, adding a supplementary blasting chamber after the main blasting chamber is standard practice for these models.
Common supplementary chamber configurations:
Manual supplementary blasting station: Operators use shot blasting guns to clean dead zones, internal cavities, and weld roots; flexible but dependent on operator skill; requires independent dust extraction and protection.
Movable auxiliary blast wheels/guns: Rail-mounted or swing-arm type, semi-automatic compensation.
Multi-angle auxiliary blast wheels: Directional blast wheels added for known dead zone orientations, achieving automatic supplementary blasting.
Selection Point: If workpieces have obvious dead zones, procurement must explicitly require a supplementary blasting chamber, and specify in the technical agreement the supplementary method, number of stations, dust extraction air volume, and lighting illuminance. Retrofit installation often involves chamber modification and dust extraction system expansion, costing far more than factory configuration.
2.4 Abrasive Circulation System
This is the “blood circulation system” of the overhead monorail shot blasting machine; its condition directly determines cleaning quality and abrasive cost:
Abrasive falls into hoppers at the chamber bottom after impacting workpieces.
Longitudinal screw conveyor collects abrasive to the transverse screw.
Bucket elevator lifts abrasive to the abrasive-dust separator at the top of the machine.
The separator separates qualified abrasive, broken abrasive, dust, and debris through air classification.
Qualified abrasive enters the storage hopper and is quantitatively supplied to each blast wheel through abrasive supply gates (pneumatic or electric) for recycling.
Separator efficiency is a core indicator: Incomplete separation causes broken abrasive and dust to return to blast wheels, reducing cleaning efficiency and accelerating blade wear.
2.5 Dust Extraction System
Shot blasting generates large amounts of dust-laden gas. Mainstream configuration is two-stage dust extraction: cyclone dust collector for primary pre-separation, cartridge (or bag) filter for secondary fine filtration, with purified discharge meeting standards. Dust collector air volume, filter area, and filter media grade must match chamber volume and abrasive circulation rate — otherwise issues such as positive pressure in the chamber, dust escape, and poor visibility will occur.
2.6 Electrical Control System
PLC centralized control with touchscreen HMI, achieving monorail speed regulation, blast wheel start/stop sequence interlocking, abrasive supply adjustment, dust extraction and abrasive circulation linkage, fault alarms, and safety door interlocks. High-end configurations can include automatic abrasive replenishment, blast wheel current monitoring (inferring whether abrasive supply is sufficient through current), and remote maintenance interfaces.
2.7 Workflow Summary
Workpiece loading and hanging → Monorail conveys into chamber → Multi-angle blasting by blast wheels (main blasting chamber) → Dead zone supplementary blasting (supplementary chamber) → Residual abrasive blow-off → Abrasive recycled through screw + elevator + separator → Dust purified and discharged through dust extraction system → Workpiece exits line or directly enters coating process
🔗 See our monorail shot blasting machine in action:Product Page
Surface cleaning of large batches of steel, iron, and aluminum castings after shakeout — removing adhered sand, residual cores, and burrs, exposing the metal surface, while providing a qualified surface foundation for subsequent magnetic particle inspection, machining, and coating.
Note: If a large amount of molding sand remains on casting surfaces before cleaning, it will accelerate abrasive contamination and separator load; floating sand should be removed as much as possible during the shakeout process.
3.2 Heat Treatment Workpiece Descaling
Scale on workpieces after normalizing, quenching, tempering, and annealing is hard and firmly adhered. Shot blasting removal is more environmentally friendly than acid pickling and more efficient than manual grinding. Simultaneously, the plastic deformation from shot blasting can introduce residual compressive stress in the surface layer, positively affecting fatigue strength improvement.
Automotive frames, specialty vehicle chassis, and construction machinery structural components — long, box-beam, multi-weld workpieces — are among the most typical applications for the overhead monorail shot blasting machine:
Remove rolled scale and rust generated during storage and transportation.
Clean welding spatter, slag, and heat-affected zone oxidation colors.
Eliminate some welding residual stress, improving fatigue life.
Provide uniform rough anchor pattern surface for electrophoretic coating, powder coating, and painting.
Compared with a roller conveyor shot blasting machine, the monorail model reaches the bottom flange and inner webs of a box beam far more effectively, because the workpiece hangs free and can rotate.
3.4 Extra-Large Workpieces Such as Coal Mine Hydraulic Supports
Coal mine hydraulic supports (top beams, bases, shield beams, linkages) are heavy, large, and have multiple internal cavities, hinge holes, and shadowed dead zones formed by reinforcing ribs — representative workpieces requiring the “main blasting chamber + rear supplementary blasting chamber” combined process. Such applications have high requirements for single-hook load capacity, chamber cross-section dimensions, monorail load-bearing capacity, and supplementary blasting station configuration.
Similar workpieces include: Large construction machinery structural components, wind turbine hubs and bases, marine supporting components, pressure vessel heads, mining machinery components, etc.
Remove rust, scale, old paint film, oil residue, and welding slag to achieve the cleanliness grade required for coating. The commonly used domestic standard is GB/T 8923.1 (equivalent to ISO 8501-1):
Grade
Name
Surface Condition
Corresponding International/Industry Code
Sa1
Light blast cleaning
Remove loose contaminants; firmly adhered scale and old paint allowed
SSPC-SP7
Sa2
Thorough blast cleaning
Scale and rust basically removed; slight shadows allowed; defect area ≤33%
SSPC-SP6
Sa2.5
Very thorough blast cleaning (near-white)
No visible oil, scale, rust, coating, or foreign matter; only point or stripe slight discoloration allowed; residual area ≤5%; uniform gray-white
SSPC-SP10/NACE No.2
Sa3
Blast cleaning to bare steel
Completely expose metal surface; no residue
SSPC-SP5
The most commonly used acceptance grade for heavy-duty anti-corrosion coating and powder coating is Sa2.5.
② Formation of Uniform Surface Roughness (Anchor Pattern)
Shot blasting creates microscopic peaks and valleys on the metal surface, i.e., “anchor pattern.” Its functions are:
Mechanical interlocking: Paint penetrates into anchor pattern valleys and cures, forming mechanical interlocking that greatly improves adhesion.
Increased effective surface area: Actual contact area per unit area increases, enhancing molecular forces.
Reduced sagging and shrinkage: Moderately rough surfaces help paint spread evenly.
Roughness is not “the greater the better.” Excessively deep anchor patterns cause insufficient paint coverage at peaks, resulting in “peak whitening” and early pitting; excessively shallow anchor patterns result in insufficient adhesion. Industry reference ranges:
Application Scenario
Roughness Reference Range
General industrial coating
45–75 μm
Anti-corrosion coating process
50–70 μm
Epoxy coatings
30–75 μm
Rubber lining substrate
Ra 25–60 μm (commonly ~40 μm)
Key Principle: Roughness must be less than about 1/3 of the coating dry film thickness, otherwise peaks may be penetrated. After selecting the powder coating or paint system, obtain the recommended roughness from the coating supplier and work backward to determine abrasive particle size.
③ Process Benefits of Line Integration
Directly entering the powder coating/painting process after shot blasting avoids flash rust during “shot blasting → transfer → placement → spraying.” Steel surfaces are highly active after shot blasting; visible flash rust can appear in tens of minutes to hours in humid environments; once flash rust occurs, re-treatment is required. Line integration compresses this time window to a minimum — an important guarantee for coating quality stability.
Connection details to consider for line integration:
The transition section length between the blasting chamber exit and coating inlet must accommodate blow-off, inspection, masking (protecting non-coated areas), and cooling.
Blow-off devices must be effective — abrasive remaining on workpiece surfaces, internal cavities, and holes entering the powder booth or curing oven will cause coating defects and even equipment damage.
Workpiece temperature must drop below the coating’s allowable range before spraying.
Airflow direction between the blasting zone and coating zone should be designed from coating zone to blasting zone to prevent abrasive dust from contaminating wet paint surfaces or powder booths.
The same type of equipment, after changing abrasive, adjusting projection speed and coverage, can be used for shot peening strengthening of gears, springs, crankshafts, connecting rods, and other parts — forming a residual compressive stress layer on the surface to improve fatigue strength and stress corrosion resistance. Strengthening processes have far higher requirements for abrasive particle size uniformity, hardness, coverage (typically requiring ≥99.7%, industry reference), and control precision than ordinary cleaning, requiring Almen test strips and arc height measurement and other testing methods.
Aluminum alloy, stainless steel, and carbon steel mixed lines (abrasive cross-contamination causes electrochemical corrosion; must separate lines or change abrasive)
Pre-coating treatment parts requiring rust removal, descaling, texturing
Workpieces with large amounts of oil not pre-treated (should be degreased first)
4.1 Information Checklist to Collect Before Selection
Most selection errors stem from incomplete preliminary information collection. It is recommended to fill in the following table before inquiry:
Category
Content to Clarify
Workpiece
Name, material, maximum/minimum single-piece dimensions (L×W×H), single-piece weight, shape features (internal cavities, dead zones, thin walls), initial surface condition (rust grade, sand adhesion, oil, old paint)
Process objectives
Required cleanliness grade (Sa2/Sa2.5/Sa3), target roughness range, whether strengthening is required, whether stress relief is required
Capacity
Shifts (1/2/3), pieces or tons per hour or per shift, peak vs. average difference, 3–5 year capacity planning
Downstream process
Whether connecting to powder coating/paint line, coating cycle time, curing oven inlet temperature limit, available transition section length
Factory conditions
Available L×W×H (especially clear height), floor load capacity, whether pit excavation is allowed and depth, power supply capacity, compressed air pressure and flow, dust emission requirements
Hanging method
Hanging point positions, fixture type, whether rotation is required, fixture rotation radius
Other
Investment budget, delivery time, local environmental and safety requirements, spare parts supply
4.2 Core Parameter Selection by Item
(1) Single-Hook Load Capacity & Maximum Workpiece Dimensions
These two parameters determine chamber cross-section, monorail specifications, and fixture design, and are first-priority parameters.
Single-hook load: Common specifications cover hundreds of kilograms to several tons; typical single-hook loads for step-type monorail shot blasting machines include 300/500/800 kg grades (industry reference); heavy hydraulic support workpieces require selection based on actual single-piece weight with safety margin.
Maximum workpiece dimensions: Chamber internal cross-section should leave sufficient clearance on all sides relative to the maximum workpiece outline to ensure abrasive projection space and prevent workpiece interference with chamber wall liners; also consider the rotation envelope circle when fixtures rotate, not just static outline dimensions.
Always leave margin: Select based on “the largest workpiece that may appear in the future” rather than “current typical workpiece”; once the chamber is built, it cannot be expanded.
(2) Conveying Mode Selection
Production Characteristics
Recommended Mode
Single product variety, uniform cycle time, extremely large batches
(3) Blast Wheel Quantity, Power & Blasting Capacity
This determines cleaning capability.
Quantity and arrangement: The more complex the workpiece and the more shadowed surfaces, the more blast wheels required. Main blasting chambers typically require arrangement from left, right, top, bottom, front, and rear directions to ensure coverage; large structural components often require 4 or more wheels.
Blasting capacity (kg/min): The blasting capacity of a single blast wheel determines the projectile energy per unit time. Cleaning efficiency is positively correlated with “total blasting capacity × projection speed.”
Total power estimation: Total machine power is mainly composed of blast wheel motors, elevator, screw conveyor, dust collector fan, and monorail drive; blast wheels account for the largest share. Total power for same-class monorail machines ranges from tens to over one hundred kilowatts (industry reference).
How to judge if sufficient: Do not rely solely on nameplate power; require the manufacturer to provide projection simulation diagrams or projection coverage analysis, and conduct full-load process tests with actual workpieces during acceptance, measuring the minimum cycle time to achieve Sa2.5.
(4) Monorail Conveying Speed
Speed range: Common operating speeds for monorail models are in the 0.3–3 m/min range (industry reference), must be steplessly adjustable.
Relationship between speed and cleaning quality: Slow speed → longer abrasive exposure per piece → more thorough cleaning but lower capacity; fast speed → higher capacity but may not achieve grade requirements.
Correct approach: First determine the “minimum effective speed” based on target cleanliness grade and measured results, then work backward to determine capacity, rather than setting capacity first and compressing time.
Heavy rust, thick scale, strengthening workpieces: low speed; light rust, texturing only: relatively high speed.
Main blasting chamber length must ensure workpieces stay in the effective projection zone long enough.
Workpieces with dead zones must have supplementary blasting chambers (see 2.3), and the technical agreement must specify supplementary method, number of stations, independent dust extraction air volume, lighting illuminance, operating platform, and protection.
Increased chamber length synchronously increases monorail length, fixture quantity, and investment; balance between coverage and cost is required.
Conventional profiles, general structural components
1.0–1.5 mm
Thick plates, heavy parts, strengthening parts
1.2–2.0 mm
By Hardness (Industry Reference)
Workpiece Material/Purpose
Recommended Abrasive Hardness
Carbon steel conventional cleaning
HRC 40–45
Stainless steel, aluminum alloy
HRC 35–40 (low hardness, reduce embedding and scratching)
Surface strengthening
HRC 48–55
Abrasive Shape Selection
Steel shot (spherical): High impact energy, mainly hammering action, good cleaning efficiency, relatively gentle roughness formation.
Steel grit/angular grit: Strong cutting action, fast removal of thick scale and old coatings, deeper and rougher anchor pattern formation.
Mixed ratio: In practice, the two are often mixed to balance efficiency and surface morphology. Industry reference steel grit mixing ratio is mostly 20%–40%, determined
Continuous shot blasting line overview in a Dingtian manufacturing plant
Sourcing Notes for International Buyers
When you request a shot blasting machine price from any manufacturer or supplier, compare more than the initial quotation: blast wheel quantity and power, abrasive recovery system, dust collector capacity and the cost of wear parts over the first years of operation. Jiangsu Dingtian Rust Removal and Coating Equipment Co., Ltd. is a China source factory with shot blasting manufacturing experience since 1998, quoting factory-direct and supporting OEM / ODM customization of the monorail continuous pass-through shot blasting machine to your workpiece mix.
For an accurate quotation on the monorail continuous pass-through shot blasting machine, send your workpiece drawings or photos, the target cleanliness grade (for example Sa2.5 per ISO 8501-1) and your daily throughput; our engineers will recommend the model, blast wheel layout and environmental configuration, together with a wear-parts list. Contact us by email or WhatsApp for a tailored proposal.
{“questions”: [{“id”: “faq-q1854-0”, “question”: “What is a monorail continuous pass-through shot blasting machine?”, “jsonQuestion”: “What is a monorail continuous pass-through shot blasting machine?”, “answer”: “It is an overhead-conveyor blast cleaning system in which workpieces hang from a monorail chain and pass continuously through the blast chamber, suited to high-volume production.”, “jsonAnswer”: “It is an overhead-conveyor blast cleaning system in which workpieces hang from a monorail chain and pass continuously through the blast chamber, suited to high-volume production.”}, {“id”: “faq-q1854-1”, “question”: “Which workpieces suit a monorail system?”, “jsonQuestion”: “Which workpieces suit a monorail system?”, “answer”: “Parts that can be hung from hooks or fixtures – castings, weldments, frames and automotive components – especially where continuous flow into a painting or powder coating line is required.”, “jsonAnswer”: “Parts that can be hung from hooks or fixtures – castings, weldments, frames and automotive components – especially where continuous flow into a painting or powder coating line is required.”}, {“id”: “faq-q1854-2”, “question”: “What are the three running modes?”, “jsonQuestion”: “What are the three running modes?”, “answer”: “The conveyor can run in continuous mode, step (indexing) mode or accumulation (power-and-free) mode, selected according to takt time and workpiece mix.”, “jsonAnswer”: “The conveyor can run in continuous mode, step (indexing) mode or accumulation (power-and-free) mode, selected according to takt time and workpiece mix.”}, {“id”: “faq-q1854-3”, “question”: “How do I choose between monorail, hook type and roller conveyor machines?”, “jsonQuestion”: “How do I choose between monorail, hook type and roller conveyor machines?”, “answer”: “Monorail suits hanging parts in continuous flow; hook type suits large non-rotatable batches; roller conveyor suits plates, sections and pipes. Workpiece geometry and daily tonnage decide.”, “jsonAnswer”: “Monorail suits hanging parts in continuous flow; hook type suits large non-rotatable batches; roller conveyor suits plates, sections and pipes. Workpiece geometry and daily tonnage decide.”}]}